
 November 5, 2026
 5 mins to read
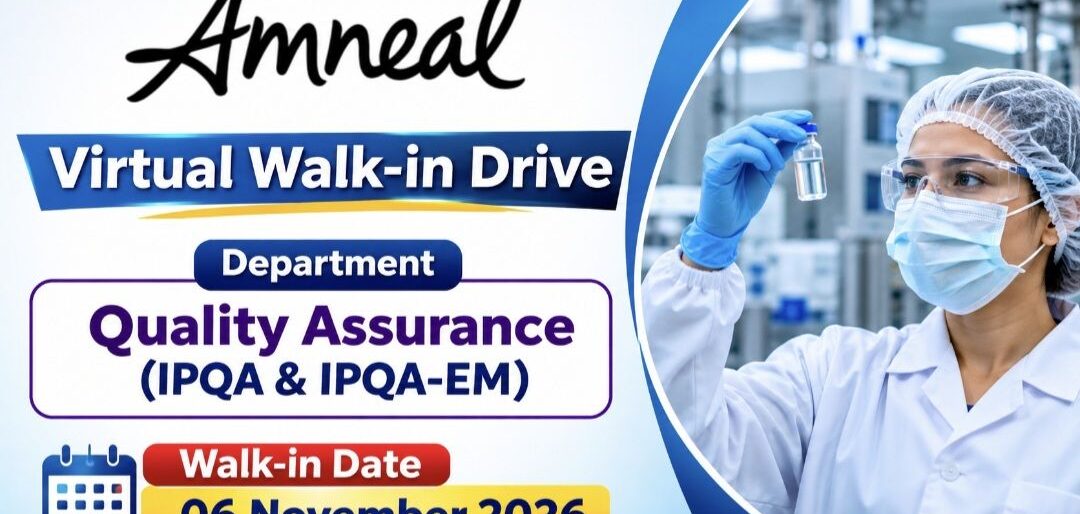
Amneal Pharmaceuticals, a globally recognized pharmaceutical company, has announced a Virtual Walk-in Drive for experienced professionals in the Quality Assurance (QA) department. The company is inviting applications for Officer/Executive positions in IPQA (In-Process Quality Assurance) and IPQA-EM (Environment Monitoring) at its injectable manufacturing facility in SEZ Matoda, Ahmedabad, Gujarat.
Candidates with relevant experience in injectable regulated manufacturing plants and expertise in pharmaceutical quality assurance activities are encouraged to apply.
Recruitment Details
- Company Name: Amneal Pharmaceuticals, Inc.
- Recruitment Type: Virtual Walk-in Drive
- Department: Quality Assurance (IPQA & IPQA-EM)
- Job Location: SEZ Matoda, Ahmedabad, Gujarat
- Interview Mode: Virtual Interview through Microsoft Teams
- Interview Date: 06 November 2026 (Friday)
- Interview Time: 09:30 AM to 03:30 PM
- Experience Required: 2–9 Years
- Designation: Officer / Executive
- Industry: Pharmaceutical / Injectable Manufacturing
1. Position: Officer/Executive – IPQA (Environment Monitoring)
Department: Quality Assurance – Environment Monitoring
Qualification:
- B.Sc. / M.Sc. (Microbiology)
- B.Pharm
- M.Pharm
Experience: 2–9 years of experience in Environment Monitoring for injectable manufacturing units.
Required Technical Skills and Responsibilities:
Candidates should have practical knowledge and expertise in the following areas:
- Environmental monitoring (EM) activities in injectable manufacturing facilities.
- Viable and non-viable particle monitoring.
- Personnel monitoring and microbiological monitoring.
- Environmental monitoring risk assessment.
- Aseptic behaviour monitoring.
- Aseptic area line clearance.
- Maintaining compliance with applicable pharmaceutical quality standards and procedures.
2. Position: Officer/Executive – IPQA (Injectable)
Department: Quality Assurance – In-Process Quality Assurance
Qualification:
- B.Pharm
- M.Sc.
- M.Pharm
Experience: 2–9 years of experience in IPQA activities for injectable manufacturing units.
Required Technical Skills and Responsibilities:
Candidates should have hands-on experience in:
- Line clearance activities in injectable manufacturing.
- In-process sampling and finished product sampling.
- Acceptance Quality Limit (AQL) inspection.
- In-process quality review of batch manufacturing and packaging logbooks.
- Shop-floor activities and quality assurance monitoring.
- Handling and monitoring of packaging areas.
- Aseptic area behaviour monitoring.
- Ensuring compliance with approved SOPs and GMP requirements.
Virtual Interview Process
Interested and eligible candidates can apply online and register for the Virtual Walk-in Drive by scanning the QR code provided in the official recruitment advertisement.
Important Instructions:
- Scan the QR code available in the recruitment advertisement.
- Complete the online application and registration process.
- Ensure that all educational qualifications and experience details are correctly submitted.
- Shortlisted candidates will receive the Microsoft Teams interview link.
- The exact interview time slot will also be shared with shortlisted candidates only.
Only candidates who successfully apply through the provided QR code will be considered for the virtual interview process.
How to Apply for Amneal Pharmaceuticals Recruitment 2026?
Eligible candidates interested in IPQA and IPQA-EM positions can apply online through the QR code mentioned in the official recruitment notification.
Applicants should keep their updated resume, educational certificates and relevant experience details ready for the selection process.
Application Deadline: Not separately specified in the advertisement. Candidates are advised to register before the scheduled interview date.
Important Disclaimer
Amneal Pharmaceuticals ensures equal employment opportunities and does not charge applicants any recruitment or employment fees. The company does not authorize any agency to collect fees for recruitment.
Frequently Asked Questions (Technical FAQs)
1. What is the difference between viable and non-viable environmental monitoring in injectable manufacturing?
Viable monitoring evaluates the presence of living microorganisms in controlled environments using methods such as active air sampling, settle plates, contact plates and surface monitoring. Non-viable monitoring measures airborne particulate matter using particle counters to assess cleanroom environmental conditions.
2. What is the importance of line clearance in injectable pharmaceutical manufacturing?
Line clearance ensures that the manufacturing or packaging area is free from materials, documents, labels and products belonging to previous batches. It prevents cross-contamination, mix-ups and product identification errors while maintaining GMP compliance.
3. What is AQL inspection in pharmaceutical packaging?
Acceptance Quality Limit (AQL) inspection is a statistical sampling method used to evaluate the quality of a batch based on predefined acceptance and rejection criteria. It helps identify packaging defects and ensures that finished products meet established quality specifications.
4. What is the purpose of personnel monitoring in an aseptic manufacturing area?
Personnel monitoring evaluates the potential microbial contamination introduced by operators during aseptic operations. It may include monitoring of gloves, gowns and other relevant contact surfaces to verify compliance with aseptic practices and contamination control requirements.
5. Why is environmental monitoring risk assessment important in sterile pharmaceutical manufacturing?
Environmental monitoring risk assessment helps identify contamination risks associated with cleanroom activities, equipment, personnel and manufacturing processes. It supports appropriate monitoring locations, frequencies, alert/action limits and corrective actions to maintain contamination control and product quality.
About Amneal Pharmaceuticals
Amneal Pharmaceuticals, Inc. (NYSE: AMRX) is a global pharmaceutical company engaged in the development, manufacturing and distribution of a diverse portfolio of medicines. The company has a team of more than 7,500 colleagues and a portfolio of over 270 high-quality medicines.
Note: This recruitment is particularly suitable for experienced pharmaceutical professionals with practical exposure to injectable manufacturing, aseptic processing, environmental monitoring and in-process quality assurance.

Leave a Comment